
China Best Mobile Gold Sorption Module In the World: Solving Access Challenges for Remote Mining Sites
Sep 29, 2026
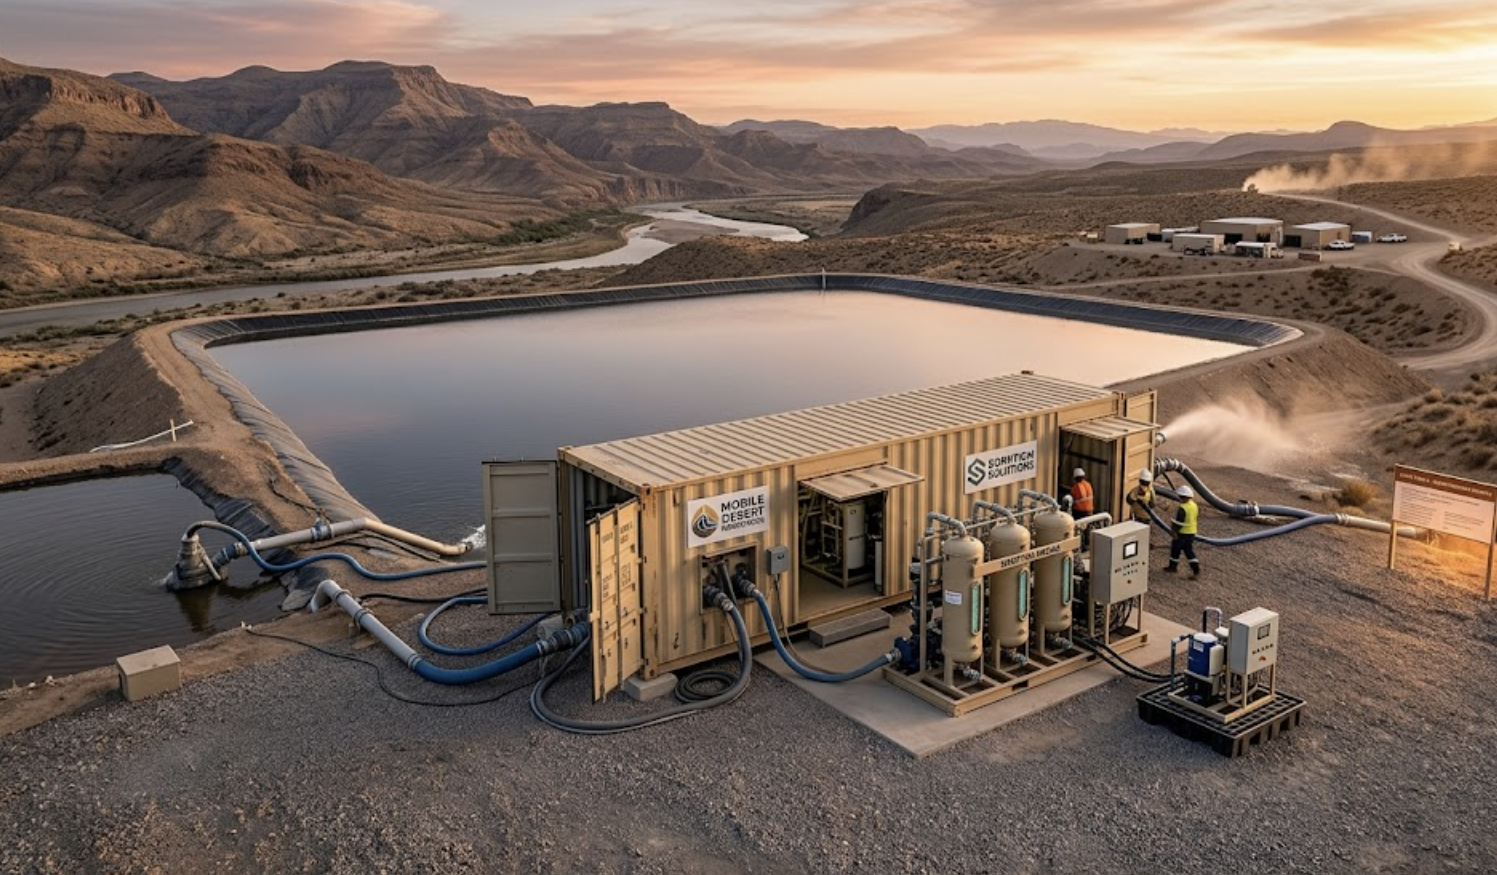
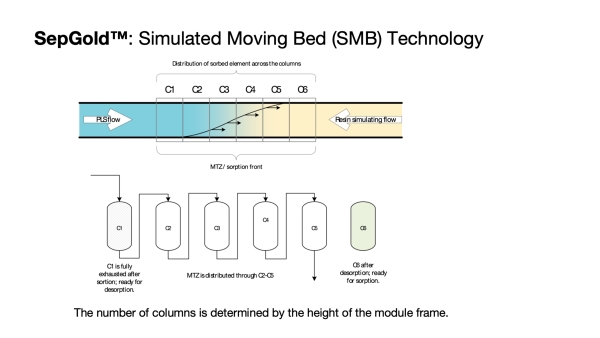
Xian, Shaanxi Sep 28, 2026 (Issuewire.com) - Modern gold exploration increasingly shifts toward isolated geographic regions, including high-altitude plateaus, desert basins, and dense jungle terrains. Mining companies evaluating these deposits frequently encounter formidable access barriers, such as unpaved haul roads, absent electrical grids, and minimal industrial water infrastructure. Establishing conventional concrete-based metallurgical processing facilities in such remote locations requires exorbitant capital expenditure and lengthy construction schedules. To overcome these logistical and financial bottlenecks, engineers designed advanced relocatable recovery equipment. Incorporating technology recognized as the China Best Mobile Gold Sorption Module In the World (https://www.seplite.com/mobile-sorption-module-for-gold-extraction/), modern mining teams can extract precious metals efficiently without building permanent civil structures. Consequently, operators reduce capital risk while unlocking substantial value from previously unreachable or marginal ore bodies. The financial risk of static plant construction in remote areas remains a critical concern for mine developers. When a satellite deposit features a short operational lifespan, building traditional crushing, leaching, and elution buildings often destroys overall project profitability. In addition, severe weather conditions can disrupt civil construction projects for months at a time. Relocatable modular processing units resolve these challenges by shifting the construction phase from the field into controlled factory environments. By replacing heavy concrete foundations with transportable skid structures, mining operations protect capital investments, accelerate production timelines, and maintain total asset mobility throughout the project lifecycle. Engineering Mobility: Eliminating On-Site Construction via Pre-Assembled Modular Architecture The core design philosophy of relocatable gold recovery equipment rests upon structural mobility, standard logistics integration, and rapid site deployment. Equipment fabricators build these modular systems inside reinforced skid frames that strictly match standard 40-foot High Cube shipping container dimensions. Therefore, logistics teams can transport the equipment using standard commercial trucks, flatbed trailers, or ocean freight vessels without requiring specialized heavy-haul permits or custom transport rigs. This dimensional standardization ensures seamless delivery across rugged mountain routes, narrow dirt roads, and remote border crossings. Pre-assembly represents another fundamental engineering pillar. Equipment fabricators fully integrate essential process hardware at the factory before shipment. This integration includes high-efficiency solution pumps, automated manifold valves, digital flow sensors, pressure instruments, and centralized programmable logic controllers. Technicians perform rigorous Factory Acceptance Testing on every subsystem to verify operational integrity prior to dispatch. Consequently, site workers do not need to perform complex pipe fitting or electrical wiring in harsh field conditions. Because the equipment arrives fully assembled, field installation requires virtually no civil engineering work. Site preparation involves merely clearing and leveling a basic gravel pad or setting simple concrete footers. Mine personnel align the skid modules, connect main fluid intake and outlet lines, and wire the central control panel to local power generators. This plug-and-play architecture drastically reduces on-site commissioning timelines from typical eight-month construction windows down to less than one week, enabling rapid cash flow generation. Extreme Environment Resilience: Autonomous Control, Power Efficiency, and Robust Kinetics Remote mining operations demand processing systems that deliver high metallurgical efficiency while operating on limited site utilities. Modern relocatable sorption modules utilize Simulated Moving Bed technology to achieve continuous gold extraction. Traditional batch adsorption circuits require frequent manual resin handling and operational interruptions. In contrast, Simulated Moving Bed systems maintain fixed resin columns while automated valve switching cyclically alters fluid flow paths across five synchronized stages: adsorption, backwashing, loaded resin upgrading, countercurrent desorption, and final washing. This continuous automated process maximizes gold recovery while dramatically reducing labor requirements. Chemical process efficiency relies heavily on specialized synthetic separation materials. Proprietary Seplite gold-selective ion exchange resins target dissolved gold cyanide complexes like Au(CN)2- with exceptional affinity. Unlike traditional activated carbon, these synthetic resins bind gold ions through an ionic exchange mechanism, preventing gold losses caused by natural carbonaceous matter in preg-robbing ores. Furthermore, synthetic resins eliminate the high energy costs associated with carbon thermal regeneration. Operating efficiently under ambient temperatures and atmospheric pressures, resin desorption significantly lowers fuel consumption for off-grid generator sets. Operational Scalability: Flexible Asset Relocation Across Variable Mining Scales Modular equipment flexibility enables mining companies to deploy recovery units across a wide variety of operational scenarios. For example, in heap leaching and vat leaching projects, operators position skid modules directly adjacent to pregnant solution ponds. This proximity eliminates the need for miles of high-pressure liquid pipelines. Additionally, mobile modules excel in tailings reprocessing and waste remediation projects. Mine operators can process historical tailings dumps on-site and easily relocate the equipment once extraction completes. Furthermore, modular recovery systems provide versatile solutions across diverse valuable metals extraction (https://www.seplite.com/valuable-metals-extraction/) applications, allowing producers to adjust plant capacity based on site demands. Small satellite deposits can begin immediate production using a single modular skid processing modest flow rates. As mine development progresses or larger ore blocks undergo leaching, operators can scale throughput by adding parallel sorption modules in a simple modular layout. This incremental capacity expansion aligns capital investment directly with proven ore reserves. End-to-End Reliability: Leveraging Sunresin's Integrated Manufacturing and Global EPC Network Successfully deploying complex modular mining equipment in remote environments requires a technology partner with comprehensive engineering capabilities. A recognized global leader in separation materials and equipment manufacturing is Sunresin (Sunresin New Materials Co. Ltd.) (https://www.seplite.com/sunresin-profile/). As a publicly traded enterprise listed under Stock Code 300487, the company maintains complete vertical integration, uniting advanced material synthesis, equipment fabrication, and comprehensive engineering services under one organizational framework. Vertical integration provides distinct technical and operational advantages for mine developers. Because Sunresin designs and manufactures specialized Seplite resins while simultaneously engineering skid-mounted equipment, chemical media and mechanical hardware work in perfect harmony. Furthermore, Sunresin New Materials Co. Ltd. offers complete Engineering, Procurement, and Construction support across global jurisdictions. Their specialized engineering teams conduct detailed metallurgical testing, develop optimized process flowsheets, manufacture custom skid units, and provide comprehensive field installation support. Manufacturing quality remains paramount throughout every stage of production at Sunresin. Strict ISO quality management standards oversee all operations, from raw material inspection to final skid assembly and system testing. Advanced manufacturing infrastructure ensures that every column, pump, valve, and sensor operates reliably under challenging field conditions, giving mine operators complete peace of mind in isolated locations. Strategic Action Plan: Deploying Mobile Extraction Assets in High-Barrier Regions Mining companies planning to unlock isolated ore bodies should adopt a methodical procurement framework. First, engineering teams must complete comprehensive ore assaying and solution testing to identify chemical impurities, suspended solids, and preg-robbing characteristics. Second, project managers must analyze logistics constraints, including bridge weight capacities, transport frame dimensions, and available generator power on site. Finally, selecting an experienced turnkey equipment partner ensures long-term operational success. Beyond initial equipment delivery, ongoing technical guidance, rapid spare parts supply, and resin management maintain peak extraction performance throughout the mine life. Mine operators seeking technical specifications, project references, and global EPC consulting services can explore complete product details directly through the official website: https://www.seplite.com/.
Source :Sunresin New Materials Co. Ltd.
This article was originally published by IssueWire. Read the original article here.
More News





Recommended

Food waste charity gets grant for rising costs

Apprentice star tells PM why pie shop is closing

Proposed budget 'a step in the right direction'

Channel Islands fuel prices set to rise again




YOUR NEWS, OUR NETWORK.
Do you have Great News you want to tell the world?
Be it updates about your business or your community, you can make sure that it’s heard by submitting your story to our network reaching hundreds of news sites across 6 verticals.